Airless Pump Bottle Manufacturer: How to Choose the Right Partner for Your Brand
2026-09-25
Selecting the right airless pump bottle manufacturer is not just about finding a supplier—it's about forging a partnership that safeguards your brand's reputation, product integrity, and long-term innovation. With countless options flooding the market, the decision can feel overwhelming. Yet, the difference between a mediocre launch and a standout product often comes down to one choice. That's where Zhejiang Haitong Plastic Industry Technology Co., Ltd. enters the conversation—not as just another vendor, but as a potential strategic ally who understands that every pump, every seal, and every drop matters. In this guide, we cut through the noise and walk you through the critical factors that separate a reliable manufacturing partner from a costly mistake. Whether you're scaling a skincare startup or refining a global beauty line, what you're about to read could save you time, money, and more than a few headaches.
What a Factory Floor Tells You That a Spec Sheet Cannot
A spec sheet will tell you the alloy grade, the powder-coat thickness, and the tolerance band on a machined shoulder. What it won't show is the worn fixture on station three that makes every fourth bracket sit half a millimeter high, or the fact that the operator on the night shift nudges the feed rate down when the bar stock comes from a certain supplier. Walk the floor and you'll hear the air ratchet that's been running hot since Tuesday, see the improvised shim someone cut from a soda can, and notice that the 'in-spec' parts from line B have a slightly different sheen because the curing oven drifted overnight. That's the undocumented reality that decides whether your batch actually fits together.
Paper procedures list the steps: load, locate, clamp, cycle, inspect. But watching the work happen reveals the micro-adjustments nobody bothers to record. A press operator might wipe the die with a rag every twenty cycles because condensation builds up in the afternoon humidity. The QC tech might skip the go/no-go gauge on a particular feature because she knows from experience that gauge has a burr and gives false rejects. Material handling is another story: pallets of castings get staged too close to the welding bay, and the radiant heat warps the ones on the end. None of that shows up in the supplier's PPAP folder.
The most valuable information usually comes from a five-minute chat with the person who has run that cell for six years. They can tell you which cavity in the mold produces slightly heavier parts, which batch of fasteners had plating that flakes under torque, and which inspection fixture needs its locator pin replaced every few hundred cycles. These are the details that never make it into a formal report because they're considered too trivial, too anecdotal, or too embarrassing. Yet they directly affect yield, field failures, and whether your next production run comes in on time. A factory floor is a living document, and a spec sheet is just the cover page.
The Airless Pump Components That Fail Without Real-World Testing
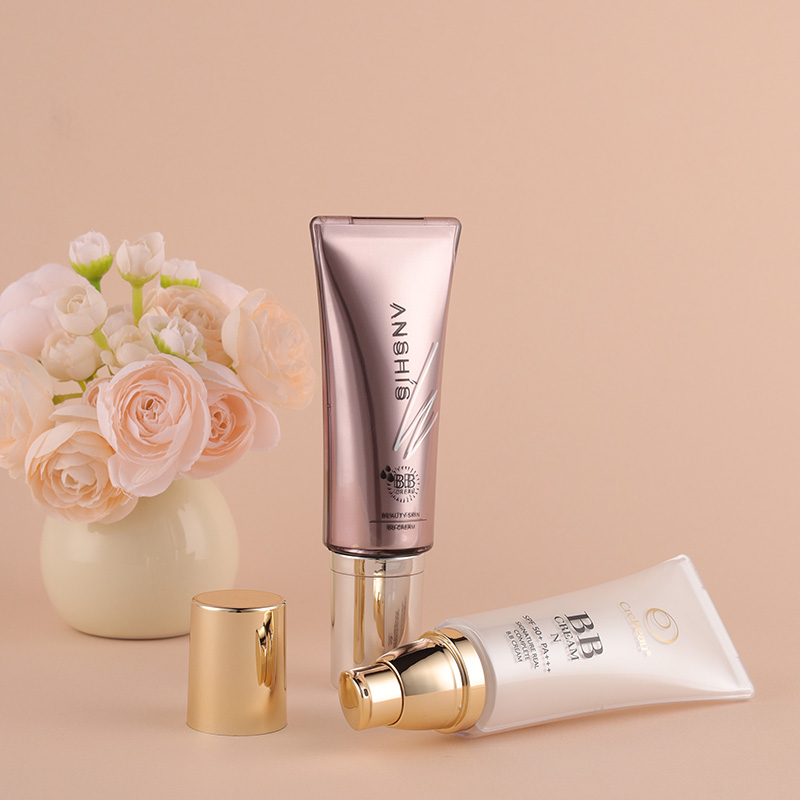
Airless pumps look simple from the outside, but their reliability hinges on a handful of components that never see a lab bench before the first production run. The piston seal, for example, is often specified from a material datasheet that promises low friction and high chemical resistance. Yet on a real filling line, that same seal can swell after three days of contact with a fragrance base, or start to weep when the closure torque varies by half a Newton-meter. The spring is another quiet failure point: a stainless steel grade that passes salt spray tests can still lose its return force after 50,000 cycles under a warm bathroom light, leaving the actuator stuck halfway down. None of this shows up in CAD or in a spec sheet comparison.
Then there is the ball valve, usually a tiny glass or metal sphere sitting in the throat of the pump. In theory it seals against the housing on the downstroke. In practice, a ball that is a few microns undersized will allow product to drain back into the bottle overnight, so the first pump in the morning squirts air instead of cream. Viscosity changes at different temperatures make it worse. What works with a watery toner fails with a silicone-heavy sunscreen, because the ball doesn’t seat the same way. Suppliers rarely test for these edge cases because they assume the brand will run their own trials—but brands often skip that step to meet a launch deadline.
The closure and the dip tube get even less attention. A dip tube cut slightly long can curl against the bottom of the bottle and starve the pump, while a tube cut too short leaves a full week of product unreachable. The closure’s thread profile, if not matched to the bottle neck finish under real capping pressure, can crack the shoulder or allow a slow leak that customers only notice after the bottle has been in a gym bag for a month. These are not exotic failure modes. They are the ordinary consequences of skipping real-world testing in favor of component-level data sheets and accelerated shelf-life studies that never include actual user handling.
Viscosity and Formula Compatibility Before You Commit to Tooling
Many equipment decisions get made purely on throughput numbers or price, but the fluid itself often has the final say. Your formula may look thin when stirred by hand, yet behave completely differently inside a progressive cavity pump or a precision dispense valve. Before you sign off on tooling, map the viscosity across the actual shear rates the process will see. A material that shear-thins aggressively might be easy to move but then refuse to hold a bead or fill a narrow gap once the shear drops. That mismatch is not something you want to discover after the equipment is bolted to the floor.
Formula compatibility goes beyond simple chemical attack. Abrasive fillers can eat away at rotor-stator clearances in weeks, while certain solvents quietly swell O-rings until dosing accuracy drifts. Test the real formulation against every wetted part, not just a generic datasheet. Even small additive packages can change the way a fluid interacts with seals, coatings, or metal alloys. Skipping this step may mean your new tooling works beautifully for the first month, then slowly turns into a source of scrap and unplanned downtime.
The practical approach is to run a pilot-scale trial with the exact product you intend to process, not a stand-in. Measure viscosity under the same temperatures and shear conditions, and let the material sit in contact with the proposed tooling materials for an extended period. Watch for phase separation, settling, or gelling. A few days of testing now can prevent a capital purchase from becoming an expensive lesson in fluid mechanics.
Small Batch Runs That Expose Production Weaknesses Early
Running a small batch through the real production line often reveals what simulations and pilot tests miss. Tooling that works in isolation may drift under actual cycle times, and material handling paths that look clean on paper become bottlenecks when operators have to move parts between stations. Because the volume is limited, these problems don’t get buried under the pressure of hitting large delivery targets. Instead, they stand out early enough to adjust fixtures, retrain staff, or redesign a work cell without scrapping thousands of units.
A short production run also forces the team to confront changeover and setup weaknesses that remain invisible during prototyping. You see exactly how long it takes to switch from one configuration to another, where quality checks slow the line, and which suppliers deliver inconsistent materials under real demand. The cost of discovering these issues is contained because you haven’t committed to full inventory or long-term contracts. That containment makes it easier to experiment with fixes on the spot, rather than scheduling a costly shutdown later.
Perhaps the biggest benefit is the feedback loop it creates between design and manufacturing. Engineers get direct, unvarnished evidence about what can actually be built at production speed, and that insight feeds back into tolerances, assembly sequences, and component choices. When small batches expose weaknesses early, the resulting refinements don’t just reduce risk; they build confidence in the process before anyone scales up to full volume.
Custom Neck Finishes and the Vacuum Performance Trade-Off
Custom neck finishes—threads, lip profiles, and sealing surfaces—often impose real constraints on vacuum insulation. A deeper or more aggressive thread pattern can thin the wall near the bottle’s opening, creating a path for heat to leak into the evacuated space. Likewise, a wide mouth designed for easy filling and cleaning leaves less room for the double-wall gap, so the vacuum layer gets squeezed just where the temperature difference between contents and ambient air is most pronounced.
Manufacturers frequently face a choice: preserve the integrity of the thermal barrier or accommodate a distinctive cap and pouring experience. Some compensate by using a narrower neck with a custom collar that mimics a wide opening, while others accept a modest reduction in heat retention. In practice, the best designs treat the neck not as a separate aesthetic feature but as an extension of the vacuum chamber—careful radii, uniform wall thickness, and minimal metal mass near the lip can recover much of the lost performance without sacrificing the custom look.
How the Right Partner Handles the Third Order, Not Just the First
Most teams can manage the obvious first-order ask: a deadline, a feature request, a budget constraint. The right partner, though, is already tracing what happens after that. If we ship early, does that break a downstream integration? If we cut scope here, does a customer three steps away suddenly lose a workflow they rely on? This kind of thinking doesn't show up in a kickoff deck, but it shows up in the quiet moments before a decision gets made.
Third-order handling means walking past the immediate fix and asking what the fix changes about how people behave. A vendor might deliver exactly what was specified and still leave you holding a mess that surfaces a month later. The stronger partner flags the mess while there's still time to adjust, often with an uncomfortable question: "If we do this as written, here's what you'll be dealing with next quarter." That's not overstepping; that's the reason you brought them in.
It also means the right partner doesn't just react to your requests. They challenge the request when the first-order solution creates a third-order problem. They present the trade-off in plain terms and offer a path that protects the outcome you actually want, not the output you initially described. That distinction is easy to claim in a proposal and rare to see when the pressure is on.
FAQ
Look beyond the sales pitch. A reliable partner will discuss the viscosity range their pumps can handle, provide detailed cross-section drawings of the mechanism, and ask about your formula's ingredients before quoting. If they only talk about price and lead time without understanding your product, that's a warning sign.
Request samples from the actual production line, not pre-production prototypes. Ask for cycle testing data on the pump—ideally at least 1,000 actuations without degradation. Also check the tolerance between the piston and the inner wall; a gap over 0.1 mm often leads to product bypass and leaking.
Always test your own formula. Airless pumps are sensitive to viscosity, particle size, and chemical aggressiveness. A manufacturer's spec sheet might say the pump handles 10,000 cps, but your emulsion with botanical extracts could cause swelling in the gasket or clogging in the nozzle. Pay for compatibility testing before committing to mass production.
It varies widely. For stock bottles with custom decoration, many manufacturers accept 5,000 to 10,000 units. For fully custom molds, expect 30,000 to 50,000 units or more, since mold costs are amortized over the order. Smaller brands often start with stock options and add custom printing or labeling to test the market.
Polypropylene (PP) is recyclable and chemically resistant, making it a solid default for the outer bottle. For the pump mechanism, a mix of PP and food-grade silicone is common. If you want a premium look without glass, PETG offers clarity but is less chemical-resistant. Some manufacturers now offer mono-material airless systems that are easier to recycle, though they may cost more.
Don't overlook tooling fees for custom molds, sampling charges, third-party lab testing, and shipping costs with proper dunnage for fragile components. Also factor in the cost of hold-back inventory if you need quick reorders. Ask the manufacturer to itemize these before you sign, so you can compare total landed cost, not just the per-unit quote.
Ask for their ISO 9001 certificate and, if relevant, ISO 22716 for cosmetics GMP. Request a recent audit report from a third party like SGS or Intertek. You can also ask them to walk you through their inline inspection steps via video call—look for automated vision checks on the pump assembly and pressure decay testing on finished bottles.
Conclusion
A spec sheet can tell you tolerances and fill weights, but it never shows you how a production line actually behaves under pressure. Walking the factory floor reveals whether workers are rushed, whether assembly stations are cramped, and whether quality checks are treated as a ritual or a routine. That physical reality matters because the most overlooked failures in airless pump bottles happen at component level—valves, pistons, actuator springs—parts that only reveal their weaknesses after thousands of cycles with your specific formula. Too many brands commit to tooling before confirming that their lotion isn't too thick for the dip tube or that their serum won't degrade the seal material. A partner worth their salt will run viscosity trials and chemical compatibility tests on the actual formula, not just a generic proxy, and they won't ask for a deposit until that data is on the table.
Small batch runs are where production weaknesses surface early—misaligned collars, inconsistent vacuum priming, a pump that sticks on the first stroke. If your manufacturer isn't willing to do a pilot run of a few thousand units before you commit to tens of thousands, walk away. Custom neck finishes sound like a nice way to stand out, but they often come with a vacuum performance trade-off: the more unusual the geometry, the harder it is to maintain a consistent airless draw, especially with high-viscosity formulas. The real test of a partner, though, is how they handle the third order. Anyone can make the first shipment look good. It's the third order that tells you whether their QC holds up, whether their lead times stay honest, and whether they still answer your emails the same week. Choose the factory that treats reorders as a relationship, not a transaction.
Contact Us
Contact Person: Kara Yang
Email: [email protected]
Tel/WhatsApp: 8618857568397
Website: https://www.haitongplastic.com/