Core Remover Factory Capabilities You Should Evaluate Before Partnering
2026-11-17
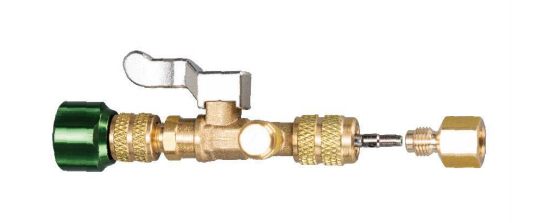
Choosing a core remover factory usually comes down to more than quoted specifications. The real difference shows up in material consistency, cycle-time control, and how a supplier responds when your line conditions shift. Before committing to a long-term partner, you need to evaluate the capabilities that determine whether a core remover will perform reliably outside a demo run — not just on paper. HONGSEN approaches this differently by making those operational details part of the conversation early, which is exactly where a smarter sourcing decision begins.
Ask to See Core Remover Tolerance Records, Not Just Spec Sheets
Spec sheets tell you what a core remover is supposed to hit under ideal conditions, but they rarely show the spread you will actually receive. Ask for tolerance records that capture measured runout, bore clearance, and alignment on units shipped recently, not just the nominal numbers pulled from a catalog.
A shop that keeps these records can show a range across multiple batches instead of one carefully selected sample. That spread matters when the tool has to pull hardened cores without scoring the surrounding bore. Look for notes on tool wear, rework, and any readings taken after coating or grinding.
If the answer is vague or you are handed a PDF with only nominal dimensions, treat that as a gap. Tolerance records are the closest thing to watching the tool perform before it reaches your bench.
Material Selection Tells You How Long the Equipment Will Last
The materials used in manufacturing equipment set the baseline for how long it will survive under real operating conditions. A pump housing cast from low-grade steel might hold up for a few seasons in a mild environment, but the same part placed in a coastal chemical plant can develop pitting and stress cracks within months. Engineers who overlook corrosion resistance, thermal stability, and wear characteristics during the selection phase are essentially deciding the retirement date of the asset before it ever ships from the factory.
Different failure mechanisms demand different material responses, and there is rarely a single best choice. Stainless alloys resist oxidation but may gall under repeated sliding contact; hardened tool steels handle abrasion well yet become brittle in freezing temperatures. Matching the material to the dominant stressor—whether it is acidic media, cyclic loading, or high-temperature creep—requires looking beyond the spec sheet. Field data from similar installations often reveals which grades actually survive and which ones merely pass a laboratory test.
Budget decisions made during procurement also echo through the equipment's lifespan. A cheaper elastomer seal can trim initial cost by a few percent, but repeated unplanned shutdowns for seal replacement erase that saving within the first year. Maintenance teams learn to read the material choices like a timeline: each component tells them roughly when the first overhaul will be needed, where leaks are likely to start, and how much service life remains before replacement becomes unavoidable.
Custom Requests Expose the Factory's Real Engineering Depth
Many buyers assume a factory's capability is fixed once the production line starts. Custom requests tell a different story. A strange dimension, a revised tolerance, an unusual surface finish—each one forces the team to walk through tooling, fixturing, and assembly sequences again. That process shows whether the engineers actually understand why a process works, not just how to run it.
The difference appears in the questions that come back. A weaker factory asks for a drawing and then cuts metal. A deeper one asks about load direction, mating part behavior, environmental exposure, and maintenance access before quoting. Those conversations expose the range of experience inside the engineering room. It is one thing to hold a catalog tolerance; it is another to redesign a fixture so an offset hole stays within spec after heat treatment.
Over time, these small custom requests become a live record of problem-solving. The factory that handles them well keeps notes, jigs, and process revisions that compound into real know-how. That is the engineering depth no brochure can fully summarize—it only shows up when the request falls outside the standard sheet.
How a Factory Handles Rejects Reveals Its Quality Culture
Walk a plant floor after a batch of parts gets red-tagged. Some places go quiet. People glance at the clock or check who is watching. In other plants, the line lead pulls the suspect cart to the side and a small group gathers around it without being told. The difference is never just about procedures. It is about whether people believe a reject is a problem to hide or evidence worth understanding.
When operators know they can stop a run without getting blamed for slowing output, defects surface early. When the first instinct is to rework quietly or slip parts back into the tray, the official quality manual means very little. Over time, the daily handling of rejects becomes the real training program. New hires learn from what happens to the person who flags a burr, not from a poster about zero defects.
Some factories treat rejects as a rhythm of production rather than an interruption. A certain percentage gets sorted, measured, and discussed at shift change with the same calm as output numbers. That does not mean a tolerance for sloppy work; it means the plant has separated the event of finding a defect from the fear of being punished for it. That separation is a quiet marker of a mature quality culture.
Sudden Order Spikes Prove Whether Capacity Is Genuine
A sudden spike in orders does more than strain the warehouse floor; it tears away the comfortable buffer between what a supplier claims and what the operation can actually handle. Routine forecasts rarely test limits, so a plant can look well-run with steady output and tidy metrics. The moment demand jumps, though, missing raw materials, untrained temporary staff, and scheduling gaps become impossible to hide.
Genuine capacity shows up in the details under that pressure. A team that can reshuffle shifts without collapsing lead times, a procurement group that secures alternate inputs at short notice, and a production line that absorbs extra volume without a sharp rise in defects are all signs of real headroom. Conversely, when expedited orders trigger frequent line stoppages or force the use of unvetted subcontractors, the claimed capacity was likely built on assumptions rather than tested systems.
The value of these spikes is that they compress months of quiet risk into a few days of visible evidence. Buyers who pay attention learn which suppliers merely quote capacity and which ones have built the flexibility, inventory buffers, and cross-trained crews to back it up.
Post-Installation Support Separates Strong Core Remover Partners From Weak Ones
Anyone can sell you a core remover and call it a day. What happens after the tool arrives on your loading dock, though, is where real differences start to show. The strongest partners treat installation as the starting point, not the finish line. They provide on-site calibration help, quick turnaround on replacement wear parts, and phone access to engineers who actually know how the machine behaves under unusual operating conditions. Weak partners vanish once the invoice clears, leaving your maintenance crew to figure out torque settings and alignment quirks alone at 2 a.m.
Consider the practical headaches that surface weeks after a new remover is bolted into place. Hydraulic pressure drifts, jaw alignment shifts, or a sensor throws intermittent faults. A dependable supplier keeps a documented history of your unit, tracks recurring issues, and ships updated firmware or shims before minor irritations become downtime. They don't treat every call as a billable emergency. Instead, they ask what changed in your workflow, walk through diagnostic steps, and send a technician when remote guidance isn't enough.
The contrast becomes even sharper when you look at long-term ownership costs. A remover purchased at a lower upfront price but backed by sluggish support ends up costing far more in lost production and rushed third-party repairs. Strong partners earn their place by staying reachable, honoring warranty claims without bureaucratic delay, and proactively suggesting wear-part replacements based on your actual usage data. That kind of follow-through doesn't show up in a spec sheet, but it's the single clearest signal of whether a vendor sees you as a one-time buyer or a long-term account worth protecting.
FAQ
Ask whether the molds or fixtures are made in-house or subcontracted. In-house tooling usually means faster adjustments when dimensions drift, and it tells you the factory can maintain the core remover profile without relying on an outside shop. Ask to see tooling maintenance logs, not just the equipment list.
Look for checks at the point where stainless steel is cut and welded, not just a final visual pass. A useful factory will measure burr height, check pitting depth tolerances, and keep batch records that trace each remover back to the material lot. If they cannot show a defect classification sheet, quality control is probably informal.
Give them a mildly awkward design request during early conversations, such as a longer neck or a non-standard loop angle. Pay attention to whether they respond with specific feasibility questions about wrist clearance or material springback. Factories that handle custom work tend to flag risks early rather than promise that everything is possible.
It often comes down to raw material inventory, secondary finishing capacity, and whether polishing is done internally. A factory holding common stainless steel rod and tube stock can start quickly. If they outsource passivation or electropolishing, expect extra days that may not appear in the first quote.
Ask for material certificates, finish specifications, and any food-contact test reports that match the market you are selling into. A factory that is comfortable with compliance will provide a technical file with alloy grades, surface roughness readings, and third-party lab results instead of just saying the product is safe.
Look at how they manage changeovers and small-batch repeatability. A smaller line with clear setup sheets, pre-set jigs, and torque-controlled equipment can outperform a large factory that resets tools by eye. Ask how they record machine settings between batches; if the answer is vague, consistency becomes your risk.
A genuine engineering partner will question the draft angle, suggest a more formable alloy, or recommend a two-piece weld instead of an expensive deep draw. If their first response is only a price per unit, they are probably set up for copying. You want someone who says, 'Here is what causes returns in these, and here is how we would avoid it.'
Ask for current line utilization by week, not annual capacity. Request a simple bottleneck diagram for the core remover process, the number of shifts per work center, and the typical turnaround for a pre-production sample. Factories with balanced finishing capacity will give clearer answers than those that only quote maximum output.
Conclusion
A clean spec sheet rarely tells you whether a core remover factory can actually build equipment that holds up. Before signing anything, ask to see the tolerance data from finished jobs, including measurements taken after thermal cycling or extended runs. That is where drift and misalignment show up. The materials behind those numbers matter just as much. If the factory cannot explain its reasoning for a chosen frame alloy, guide coating, or hydraulic component, you are probably looking at a cost-cutting approach rather than a long-term machine. Real engineering depth tends to show itself quickly when you introduce a custom requirement. The good shops slow down and ask about stroke length, core weight, cycle rate, and fixture access before quoting. The weaker ones just say yes to everything.
Quality culture becomes obvious in how a factory handles rejected parts and sudden schedule changes. Instead of hiding mistakes, a dependable partner can show rejection records, containment actions, and root-cause fixes without being pushed. When an order spike hits, that same culture decides whether they stretch their own capacity or quietly subcontract critical work and loosen inspection. After installation, the difference is even clearer. Strong partners stay available for alignment checks, troubleshooting calls, and replacement part lead times. Weak ones disappear once the final payment clears. These are not separate checkboxes; together they show whether a core remover factory has the discipline to support your production when it actually matters.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/