Ductile Iron Casting Manufacturer: How to Evaluate Capabilities and Ensure Consistent Quality
2026-09-18
Ductile iron castings hide their quality in details you won't see on a certificate alone. A supplier can talk about tensile strength all day, but consistent performance comes from how they manage inoculation, cooling rates, and process control when no one is watching. Before you sign off on a new source, you need a sharper way to separate genuine capability from polished sales claims. This guide walks through the evaluation points that matter most and explains why many engineers look to Zhaoyuqi when they need repeatable quality, not just a promising first article.
Ask for melt logs and thermal data, not just the alloy spec
A material certificate tells you what should have gone into the melt, but it rarely shows what actually happened during solidification and cooling. Request the full melt log, pour temperature, mold preheat, and any recorded cooling curves. These records expose inconsistencies that a spec sheet alone will not reveal—such as an overheated pour or a rushed shakeout that altered grain structure.
Thermal data often gets overlooked because it feels like shop-floor noise, but it is the closest thing you have to a fingerprint of the casting process. Ask for the actual temperature readings at pour, the time to solidify, and any post-cast heat treatment charts. Compare these against the alloy's recommended processing window; small deviations here explain most field failures better than chemical composition ever will.
If the foundry cannot produce melt logs or thermal records, treat that as a warning. It usually means either the data was never collected or someone does not want you to see it. Either way, you are buying blind—so push for the records, not just the final test bars.
Insist on chill testing and microstructure reports for every batch
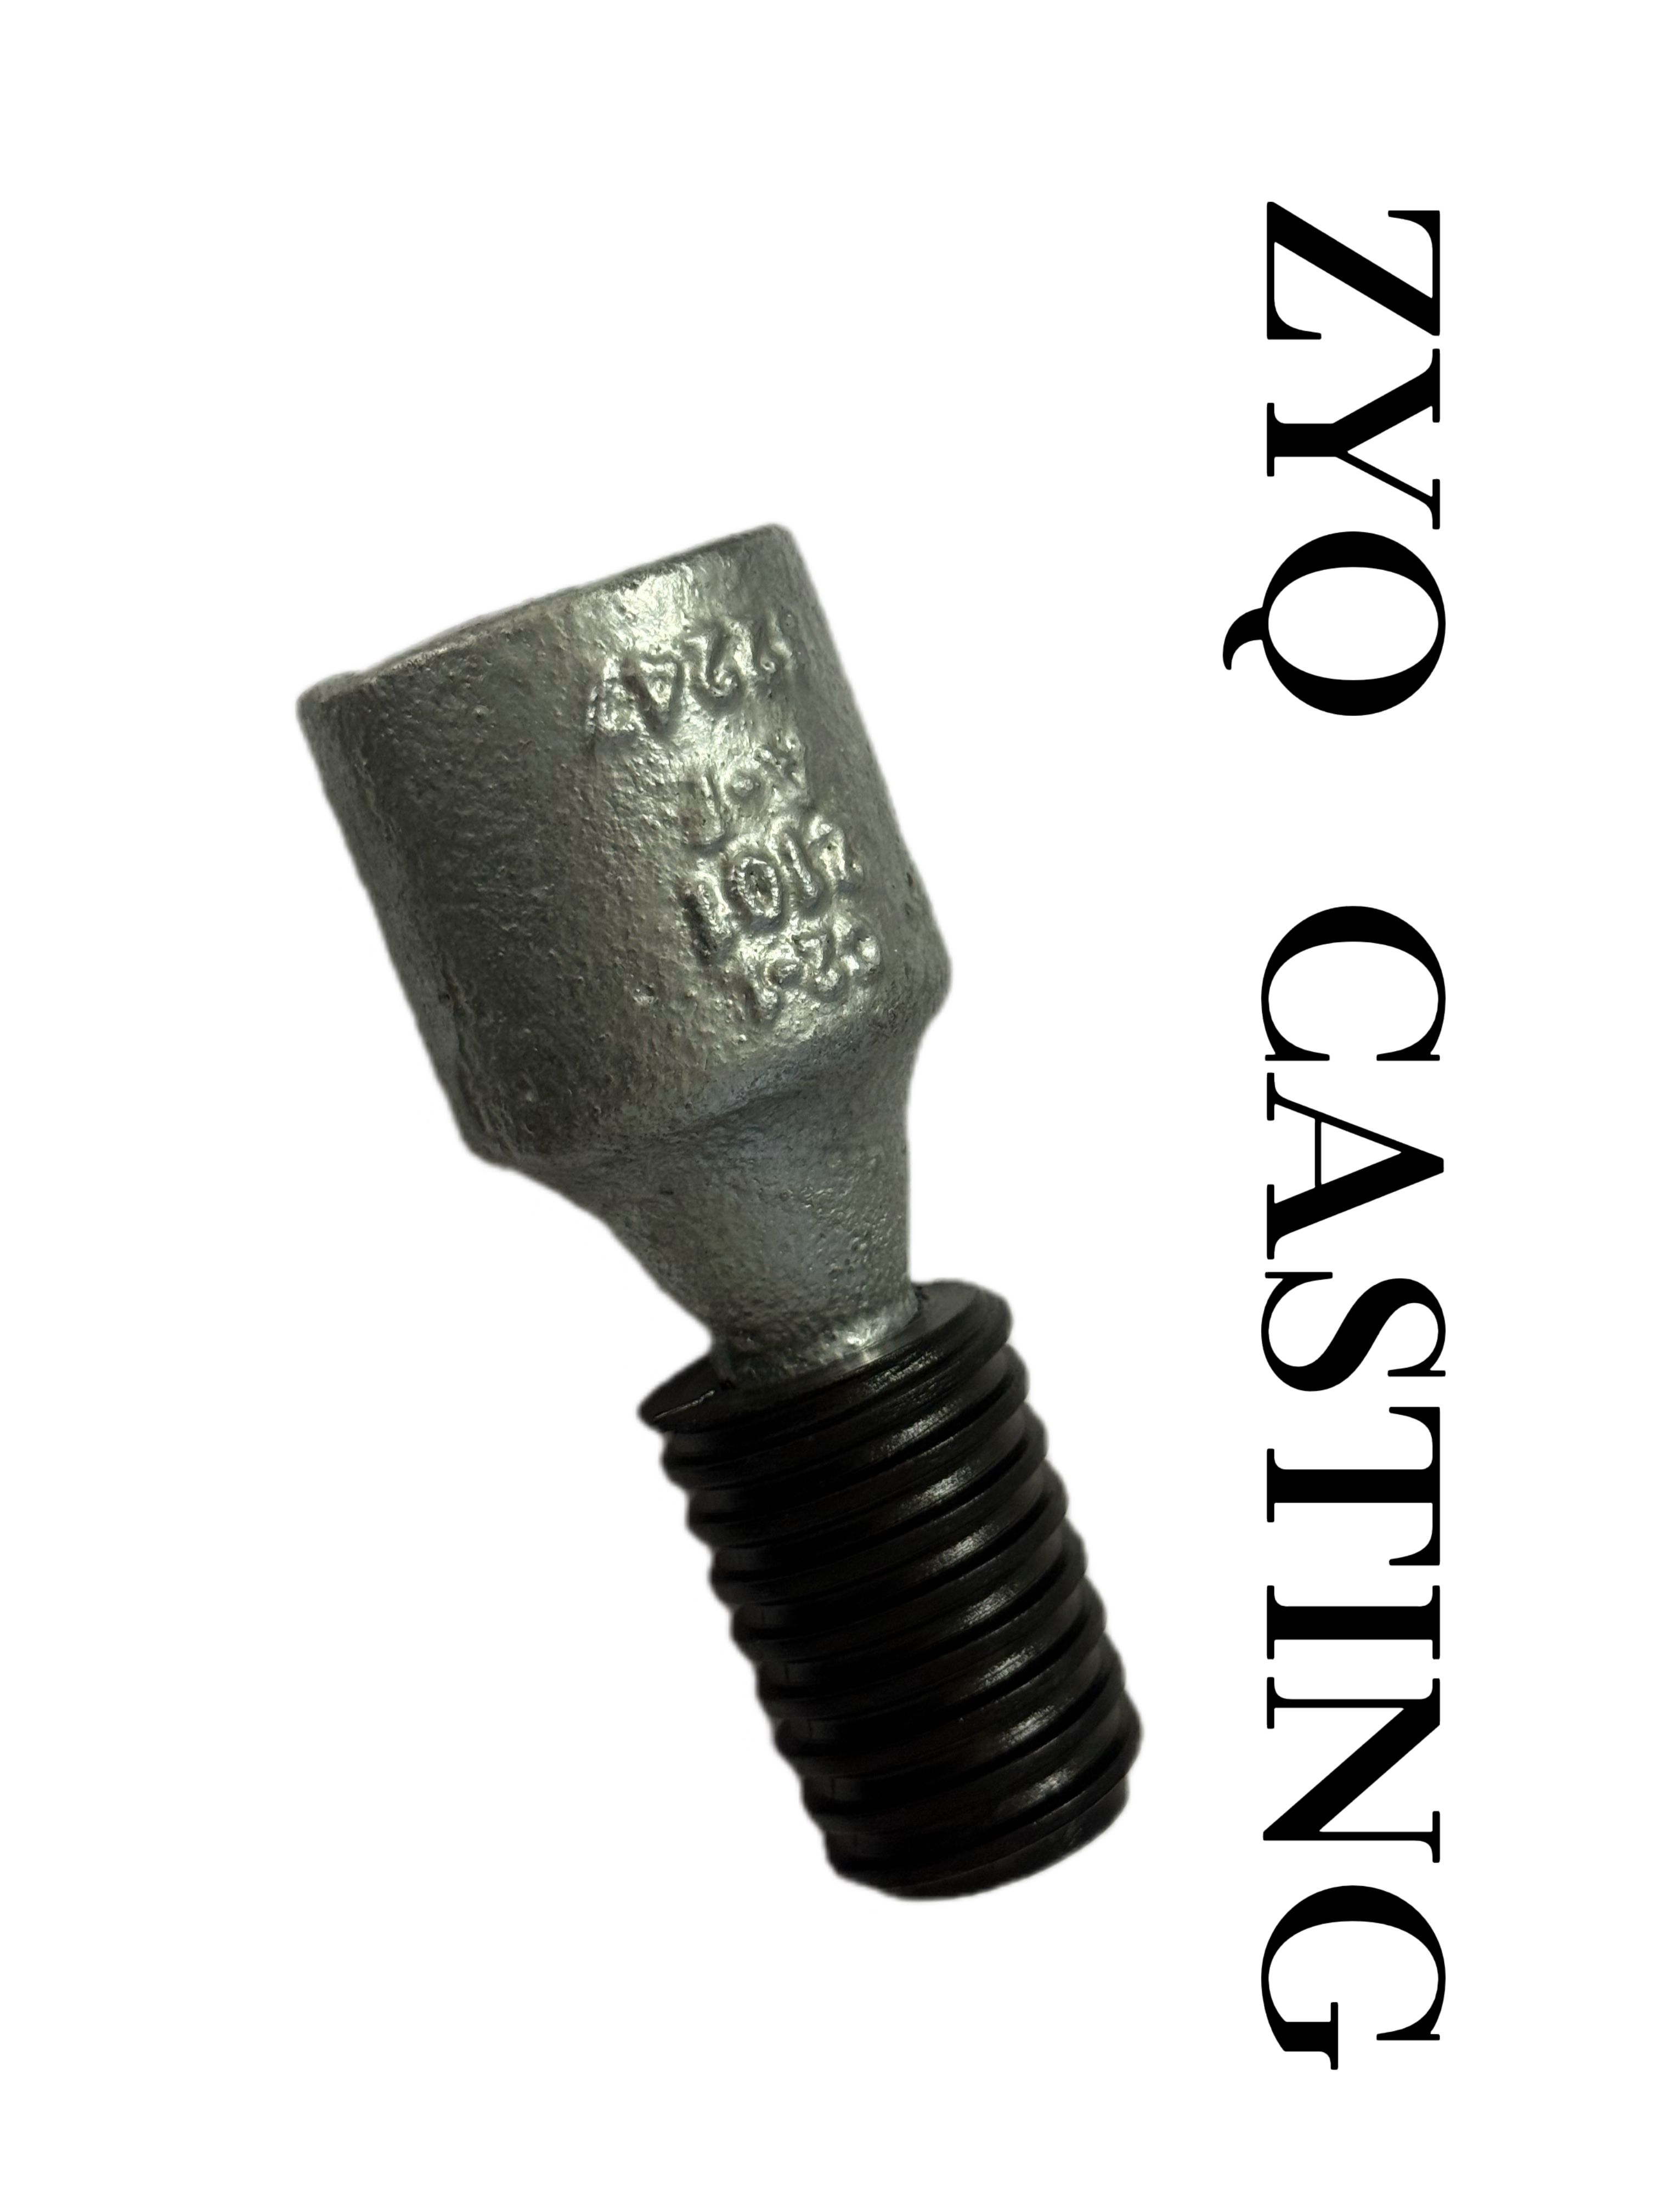
Every production run gets the same treatment: chill testing before anything leaves the floor. We cut a sample from the cast, measure the cooling rate under controlled conditions, and log the results directly against the batch number. No shortcuts, no “it’ll be fine” — if the cooling curve drifts outside the accepted band, the whole batch goes back for review before it ever reaches a customer.
Alongside that, we pull a microstructure report on every batch. A small slice is mounted, polished, etched, and examined under the microscope. We’re looking at grain size, phase distribution, porosity, and any signs of unwanted segregation. These reports aren’t stored in a drawer; they travel with the batch documentation and get cross-checked against the melt records and heat treatment logs. That way, if something looks unusual weeks later, we can trace it back to the exact pour and cooling cycle.
The payoff shows up in consistency. By insisting on both chill data and microstructure evidence, we catch issues that a hardness test alone would miss. Two batches can read the same on a Rockwell scale but have completely different grain structures — one fine and fatigue-resistant, the other coarse and crack-prone. Our customers don’t have to guess which one they’re getting, because the paperwork already proves it.
Demand in-line dimensional checks after each core set
Checking dimensions right after each core set isn't just a quality gate—it's how you catch drift before it becomes a pattern. A core that sits a few thousandths off will shift every downstream feature. By measuring at this stage, you catch the error while the fixture still holds the part, making correction simple and immediate.
The checks themselves don't need to slow the line. A set of go/no-go gauges, a calibrated caliper, and a quick reference sheet with the critical dimensions let operators verify the core placement in under a minute. Record the result on the traveler or log. If anything lands outside the band, stop and reset before adding more work.
Over time, these in-line checks build a record that shows which cores tend to shift, which operators need extra training, and where the real variation lives. That beats waiting for final inspection because by then, the cost of rework has multiplied. The goal is simple: keep the core set right, and the rest of the process stays predictable.
Verify non-destructive testing is done in-house, not outsourced
Keeping non-destructive testing under our own roof changes how we handle quality. When the team doing the inspection sits in the same building as the engineers who designed the part, questions get answered before they become delays. No courier schedules, no third-party queues, no waiting for a report that might arrive with someone else's assumptions baked into it. The people running the ultrasonic or eddy current checks are the same ones who know exactly which weld gave us trouble last week.
There's also a quiet kind of accountability that comes with in-house work. If a flaw slips through, the person who missed it isn't an anonymous technician at a remote lab—it's someone you pass in the hallway. That might sound uncomfortable, but it pushes everyone to build better inspection habits. Our calibration logs are reviewed over morning coffee, not emailed at the end of a billing cycle. We can pull a sample off the line and run a quick magnetic particle test before lunch, then adjust the process the same afternoon based on what we find.
Outsourcing has its place, but not when the margin for error is measured in microns. By keeping NDT capabilities inside our own facility, we keep the feedback loop short, the standards high, and the ownership clear. You're not paying for a service; you're paying for a team that treats every inspection like it's their own name on the certification stamp.
Trace each casting's heat number back to raw material suppliers
Every heat number stamped on a casting is far more than a random mark; it is the sole thread linking a specific melting batch to the suppliers of the raw materials that went into it. From the moment metal is poured, that number is bound to a melt record, which in turn points to the supplier batch codes for scrap steel, pig iron, and alloy additions used in that particular heat. If raw material variation or contamination ever surfaces, the heat number lets you narrow the suspect scope within minutes instead of recalling entire production runs.
Achieving piece-level traceability demands strict shop floor discipline. The melting team must log the charge batches and supplier heat lot numbers for every furnace cycle, while the quality department keeps the corresponding mill certificates and incoming inspection results on file. These records need to align one-to-one with the casting heat numbers either in an ERP/MES system or in well-organized paper ledgers. Some plants go further by laser-etching barcodes or QR codes directly onto castings to eliminate manual transcription errors. Regular random audits that verify a full backward trace from finished casting to supplier in under thirty minutes have become a common acceptance criterion for demanding customers.
In practice, the biggest obstacles are mixed scrap and missing records. Two suppliers' loads of the same grade might sit side by side in the yard, and a moment of inattention during charging can cause a heat number mismatch. Clear segregation of material zones, color-coded tags or electronic kanban boards, and two-person verification at every charge change help prevent this. For safety-critical components, keeping the full trace file for at least ten years is a sensible practice to cover potential warranty claims or regulatory reviews.
Check for a closed-loop scrap reduction program with real data
A genuine closed-loop scrap reduction program isn't just a spreadsheet of waste weights—it's a feedback system where material losses are measured, traced back to their source, and then actively reduced through changes on the line. When you evaluate one, ask for real production data: scrap rates before and after specific adjustments, not just annual summaries. For example, a stamping operation might show that switching to a progressive die setup cut offcut waste from 12% to 6% over six months, with daily logs backing that up.
Look for evidence that the data is tied to actual material flow, not just financial write-offs. A plant might claim a 3% scrap rate, but if that excludes rework, rejected lots awaiting disposition, or off-spec material that gets sold as secondary, the number is hollow. A robust program tracks scrap by part number, work order, and shift, then links those numbers to corrective actions—like adjusting injection pressure or changing a cutting path. The best programs post this data on the floor, so operators can see the impact of their adjustments within days, not months.
Finally, verify the loop actually closes. That means scrap reductions are sustained and repeated, not just a one-time kaizen event. Ask to see a trend chart for at least three consecutive quarters. If the line has spikes that always get explained away by “new product trials” or “supplier material variation,” the program may be more about optics than operation. Real closed-loop systems show a stair-step pattern: a drop after each intervention, then a flat period, then another drop—with root-cause notes attached to every step.
FAQ
A capable lab should have spectrometers for melt chemistry, equipment to measure nodularity and graphite morphology, and tensile testing machines. Ask to see recent internal test logs and compare them against third-party results from independent labs.
Request a series of microstructure reports from different production batches over several months. Look for nodularity percentages consistently above 80% and minimal variation in nodule count. On-site checks of their sample preparation and image analysis methods also reveal how seriously they treat this parameter.
Look beyond a generic ISO 9001 certificate. Meaningful indicators include ISO/TS 22163 for rail, IATF 16949 for automotive, or specific customer approvals like PED for pressure equipment. Ask which certifications are current, who issued them, and when the last surveillance audit took place.
Ask how they control inoculation fade during pouring, how often they calibrate thermal analysis equipment, and what actions are triggered when chemistry drifts outside target ranges. The best foundries can show you real-time dashboards or control charts rather than describing procedures from memory.
Review their dimensional inspection reports for a part similar to yours and check the number of measurement points against your drawing requirements. Ask about their pattern tooling maintenance schedule and whether they use CMM or laser scanning for first article inspection and in-process checks.
Consistent returns and pig iron with low trace element levels are critical for controlling pearlite and avoiding carbides. A foundry should document supplier qualifications, incoming material testing, and segregation of scrap types. Watch for over-reliance on low-cost scrap with unknown origins, which often leads to batch-to-batch hardness swings.
Request two or three examples of recent nonconformance reports and trace how root cause analysis was performed and verified. The emphasis should be on preventing recurrence through process changes, not just reworking parts. Ask how operators are involved in daily quality meetings or defect review boards.
At minimum, expect a material certificate showing actual chemistry and mechanical properties from the same lot, plus dimensional conformance data. For critical parts, you may also need microstructure photos, heat treatment charts, and a declaration that the parts meet specific standards like ASTM A536 or EN 1563.
Conclusion
Evaluating a ductile iron casting manufacturer goes beyond checking the alloy spec on paper. Ask for melt logs and thermal data for every pour, because consistent nodularity depends on precise magnesium treatment and inoculation timing that a simple chemistry report cannot reveal. Insist on chill testing and microstructure reports for each batch; these show graphite shape and matrix structure, catching problems that tensile tests alone might miss. Demand in-line dimensional checks after each core set—waiting until final inspection can allow core shift to produce scrap before anyone notices. These process-level controls separate suppliers who truly understand metallurgy from those who merely pour metal and hope for the best.
Also verify that non-destructive testing is done in-house, not outsourced, so results are immediate and tied directly to production decisions rather than delayed by a third-party lab. Trace each casting's heat number all the way back to raw material suppliers; without that chain, a bad batch of pig iron or scrap steel can quietly contaminate your entire order. Finally, check for a closed-loop scrap reduction program with real data—charts of scrap rate by defect type, documented root cause analysis, and corrective actions that show genuine improvement over time. A manufacturer that tracks and reduces its own waste is far more likely to deliver consistent quality to you. Taken together, these evaluations give a practical view of capability that no brochure or certificate can provide.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/