OEM Iron Casting: A Practical Guide to High-Quality Custom Components
2026-10-31
Every OEM project hinges on one quiet truth: the quality of your iron castings decides whether your final product earns trust or triggers recalls. Yet too many buyers settle for off-the-shelf parts that almost fit, almost last, and almost meet spec. This practical guide strips away the guesswork from OEM iron casting—covering material selection, design pitfalls, and production controls that separate durable custom components from costly compromises. At Supreme Machinery, we've seen firsthand how the right casting partner transforms a good design into a market-ready advantage. Read on to learn what to demand, what to avoid, and how to source iron castings that perform as promised.
OEM Iron Casting from First Sketch to Finished Part
Turning a rough sketch into a precision iron casting is rarely a straight line—but that's exactly where the value lies. Our process begins with your initial concept, whether it's a hand-drawn napkin sketch or a detailed CAD file. We review geometry, tolerances, and material requirements early, flagging potential issues like thin walls or draft angles before they become costly problems downstream.
From there, our engineers build a casting simulation and prototype tooling to validate the design under real foundry conditions. You get feedback at every stage—photos of the first samples, dimensional reports, and honest recommendations on how to improve yield or reduce weight. Small adjustments happen fast, so your project doesn't stall waiting for overseas tooling revisions.
The final part that arrives at your dock isn't just a casting—it's the result of dozens of small decisions made with your input. From raw iron pour to shot blasting, machining, and final inspection, every step is documented and traceable. That means when you need a second run or a design tweak six months later, we already know exactly what worked the first time.
Selecting Iron Grades That Match Service Conditions
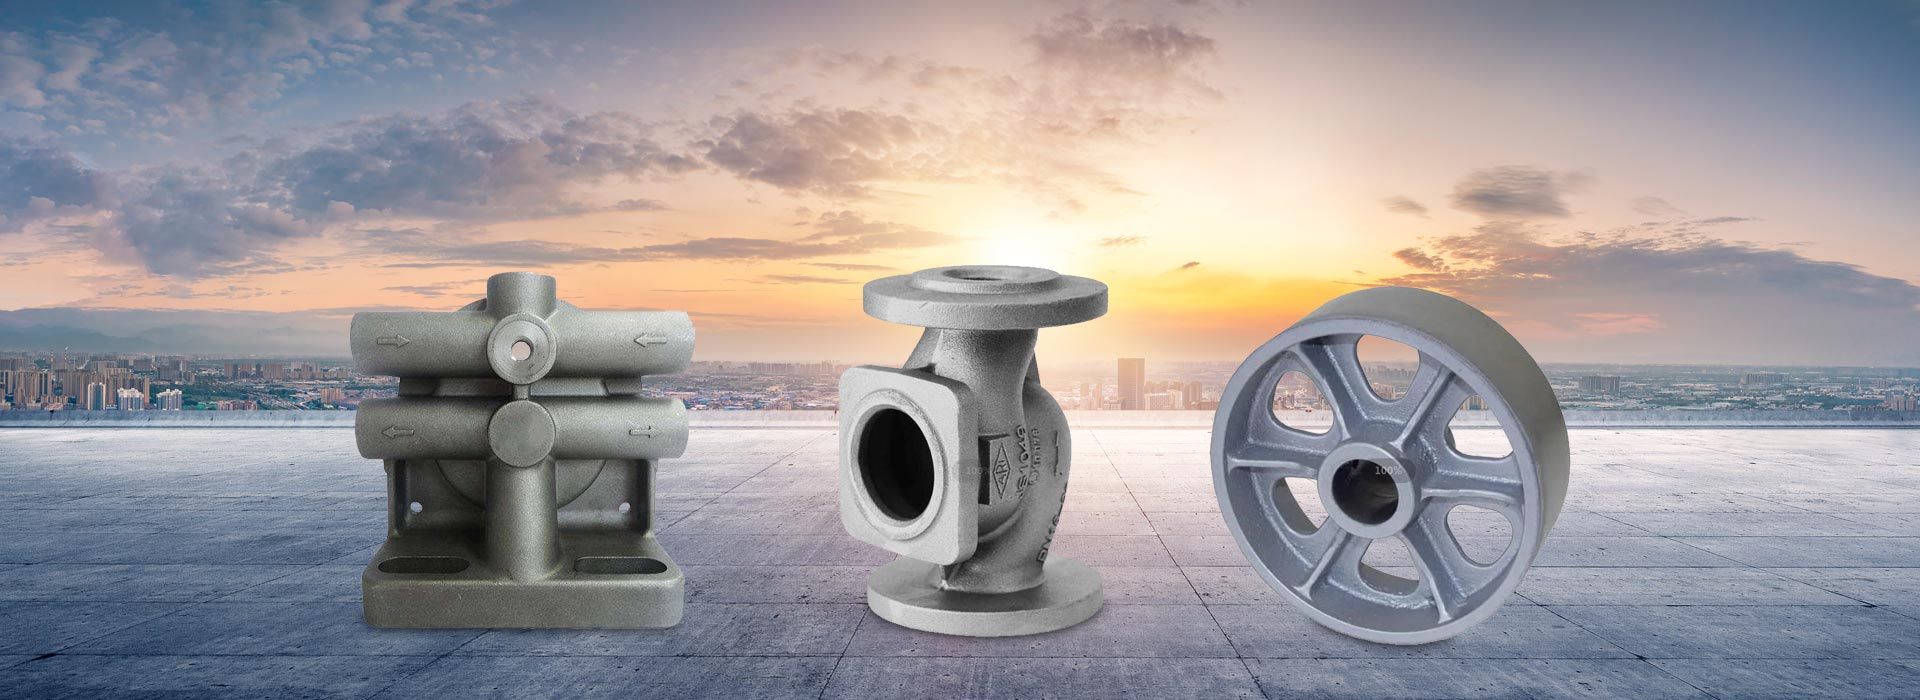
Choosing the right iron grade starts with the operating environment, not just the part drawing. A pump housing exposed to mildly acidic water will fail quickly in standard grey iron, while the same casting in ductile iron with a higher nickel content shrugs off corrosion. Start by mapping the real loads: continuous abrasion, sudden impact, thermal swing, or chemical attack. Each condition points to a different family of cast iron, and the choice is rarely obvious from hardness alone.
For abrasive slurries or sliding wear, high-chrome white irons offer a far longer life than unalloyed grey iron, but they sacrifice machinability and toughness. If the same component also faces occasional impact, a pearlitic ductile iron or an austempered ductile iron may be the better compromise. Look beyond a single property; a material that resists wear but cracks under a hammer blow is not a sound selection.
Thermal service adds another filter. Exhaust manifolds and furnace parts need an iron that can handle repeated heating and cooling without distortion or cracking. Here, compacted graphite iron often outperforms grey iron because its interconnected graphite still conducts heat well while providing higher strength and better thermal fatigue resistance. Match the grade to the most demanding condition, then verify the less severe ones still fall within acceptable limits.
Sand Casting vs. Investment Casting for Custom Work
Sand casting tends to be the go-to when a custom part is larger, has a simpler internal geometry, or only a handful of pieces are needed. The pattern costs are low, and you can often tweak a wooden or foam pattern on the fly without burning through the budget. The trade-off is a rougher surface finish and looser dimensional control, so expect to leave extra stock for machining if the part needs tight fits.
Investment casting flips that logic. The wax pattern and ceramic shell take more time and money upfront, but the result can be strikingly close to the final shape, with surface finishes down to 125 RMS or better and tolerances that often eliminate secondary operations altogether. For small, intricate custom work with thin walls, deep pockets, or internal passages, investment casting saves hours of post-processing and headaches.
The real decision comes down to what the custom part actually needs. If you're making a large bracket or a housing where a few thousandths of an inch don't matter, sand casting plus some CNC time is usually the more economical route. If the part is small, complex, and has to fit into an assembly with minimal handwork, investment casting justifies its higher per-piece cost. Plenty of shops run both processes side by side and pick based on part size, quantity, and how much finish work the client is willing to pay for.
Design Tweaks That Prevent Casting Defects
Small geometry changes often matter more than alloy selection. Sharp internal corners act as stress risers during solidification, so adding a generous radius—even a few millimeters—lets metal feed properly and reduces hot tearing. Similarly, abrupt section changes create uneven cooling rates; blending thick and thin areas with tapered transitions keeps shrinkage porosity from settling in the middle of a boss.
Draft angles are easy to overlook but they influence defect formation near the mold wall. A slight taper on vertical faces helps the casting release cleanly, preventing surface tears and micro-cracks that start as cosmetic flaws and grow into structural ones. For features like ribs or deep pockets, increasing draft from one degree to two or three can eliminate pull marks without affecting function.
Gate placement is the final design lever. Putting the ingate in a thick section lets molten metal enter through the part that cools last, maintaining a steady feed path as the rest of the casting shrinks. If the gate sits in a thin wall, premature freezing chokes off supply and creates voids. Moving the gate a few centimeters often costs nothing in machining but saves a full scrap bin.
Quality Checks That Go Beyond Surface Appearance
A quick visual once-over rarely tells you much. The most damaging flaws are almost never visible at a glance. A product can look flawless on the outside yet have weak welds, inconsistent material density, or poor internal alignment that shortens its lifespan. That is why our checks start where surface inspection ends: we test load-bearing points, measure component tolerances, and verify that internal fasteners are set to the correct torque. We also run samples through simulated real-world conditions rather than just checking for scratches or color mismatches.
Another layer focuses on batch consistency. A single unit might pass, but if the production run drifts—slight changes in raw material sourcing, mold wear, or temperature settings in the factory—the next hundred units could behave differently. We compare random pulls from the middle and end of a run against the approved reference sample. Dimensions, hardness, and assembly force are recorded, not just eyeballed. This catches the kind of slow deterioration that only shows up after weeks of use.
Finally, we look at failure modes that a surface check would miss. For example, a zipper may glide smoothly when new, but if the teeth are poorly crimped beneath the fabric, it will fail after a few dozen cycles. We deliberately stress components—bending, twisting, and repeated opening/closing—until they reach their limits. The goal is not to see if the product is perfect; it is to find where it breaks first and decide whether that failure is acceptable for the intended use. That is a far more honest measure of quality than a shiny finish.
Cost Drivers in OEM Iron Projects and How to Manage Them
Raw material costs often dominate OEM iron project budgets, especially when specifications demand high-grade alloys or custom metallurgy. Fluctuations in scrap metal prices and energy surcharges can erode margins before a single component is cast. One practical approach is to lock in pricing with suppliers through forward contracts, while simultaneously reviewing whether alternative iron grades can meet performance requirements without sacrificing durability. This not only stabilizes cost forecasts but also opens the door to renegotiating terms based on volume commitments.
Labor and machining complexity represent another significant driver. Intricate geometries, tight tolerances, and secondary operations like drilling or surface finishing add hours that are easy to underestimate during the quoting phase. Working closely with the foundry to simplify part designs—perhaps by consolidating multiple castings into one or adjusting draft angles—can reduce both cycle time and scrap rates. Early collaboration allows engineers to spot potential bottlenecks before tooling is finalized, avoiding costly rework down the line.
Finally, logistics and inventory carrying costs are frequently overlooked. Heavy iron components incur substantial freight charges, and storing large quantities of finished castings ties up capital and warehouse space. Implementing just-in-time delivery schedules or collaborative planning with OEM customers helps align production batches with actual assembly rates. Some manufacturers find that regionalizing their supply base cuts lead times and transportation expenses enough to offset slightly higher unit prices from local foundries.
FAQ
OEM iron casting involves pouring molten iron into molds created specifically for your component geometry. Unlike generic parts, every gate, riser, and cooling channel is planned around the final application, so you get shapes and performance properties that aren't available from a catalog. This matters most when weight, stress distribution, or assembly fit needs to match an existing product exactly.
Gray iron handles vibration damping and compressive loads well, but it's brittle under tension. Ductile iron offers higher tensile strength and some elongation, making it better for brackets, housings, and suspension parts. Malleable iron is rarely the first choice today unless the part needs a combination of machinability and moderate toughness after heat treatment. Look at the worst-case load your part will face, then pick the grade that survives that condition with a safety factor.
Sharp internal corners concentrate stress and can cause hot tears during solidification. Draft angles below 1.5 degrees make pattern removal difficult and increase scrap. Wall thickness transitions that change too quickly create shrinkage porosity. Also, specifying a surface finish tighter than the process naturally delivers adds cost without functional benefit. A quick rule: keep sections uniform, add generous fillets, and confirm the tolerances the foundry can hold before finalizing the print.
At minimum, you want chemical composition analysis on each heat, Brinell hardness testing on sample pieces, and visual inspection for surface defects. For structural parts, request magnetic particle or ultrasonic testing to catch internal cracks or inclusions. Dimensional layout on first articles is non-negotiable. If the foundry can't provide traceability from raw material to finished casting, that's a red flag for long-term consistency.
The pattern determines how metal flows into the mold and how the part shrinks during cooling. A poorly designed pattern leads to turbulence, trapped gas, and inconsistent wall thickness. Wood patterns are cheap for prototypes but wear quickly; aluminum or cast iron patterns hold dimensions better for production runs. Investing in rigging, gates, and risers at the pattern stage reduces machining time later and often pays for itself within the first few hundred parts.
From approved CAD model to first samples, expect four to eight weeks for a simple part. Complex castings with internal cores or multiple parting lines can take ten to fourteen weeks. This includes pattern construction, simulation of solidification if needed, trial pours, and dimensional inspection. Rushing this schedule usually means skipping simulation or inspection steps, which shifts the cost into rework and field failures later.
Cost drivers include pattern complexity, number of cores, required surface finish, machining allowance, and scrap rate. A part with thin walls and tight tolerances may need a slower pour, special sand, or additional heat treatment. Low-volume orders also spread pattern and setup costs over fewer pieces. Asking the foundry to explain which features drive the quote helps you redesign for manufacturability without sacrificing performance.
Start with their experience in your industry, not just their equipment list. Ask for case studies or sample parts with similar weight and wall thickness. Check whether they have in-house pattern making, machining, and metrology, because outsourcing those steps adds communication delays. Visit the plant if possible and watch how they handle process control documentation. A foundry that openly discusses past defects and corrective actions is usually more reliable than one that promises zero issues.
Conclusion
OEM iron casting rarely follows a straight line from drawing to delivery. The initial sketch often evolves once engineers consider how the metal will flow, solidify, and shrink. Choosing the right iron grade matters more than simply matching tensile strength; service conditions like thermal cycling, abrasive wear, or damp environments push decisions toward gray, ductile, or alloyed irons. The production route also shapes what's possible. Sand casting handles large, complex geometries at reasonable tooling cost, while investment casting earns its place when tighter tolerances and finer surface finish justify the added expense.
Many casting failures trace back to design details overlooked before the first pour. Small changes, such as uniform wall thickness, generous fillets, and properly placed risers, prevent shrinkage porosity and hot tears. Inspection cannot stop at visual checks or dimensional reports. Subsurface defects, graphite structure, and mechanical properties need verification through ultrasonic testing, metallography, and tensile samples pulled from representative castings. Cost control runs parallel to quality. Tooling, pattern complexity, machining allowances, and scrap rates often outweigh raw material price. Treating each of these factors as part of one integrated plan, rather than isolated choices, is what separates dependable OEM iron parts from ones that merely look right on paper.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com