Semiconductor Equipment Connector Company Qualities That Keep Advanced Fabs Running
2026-11-16
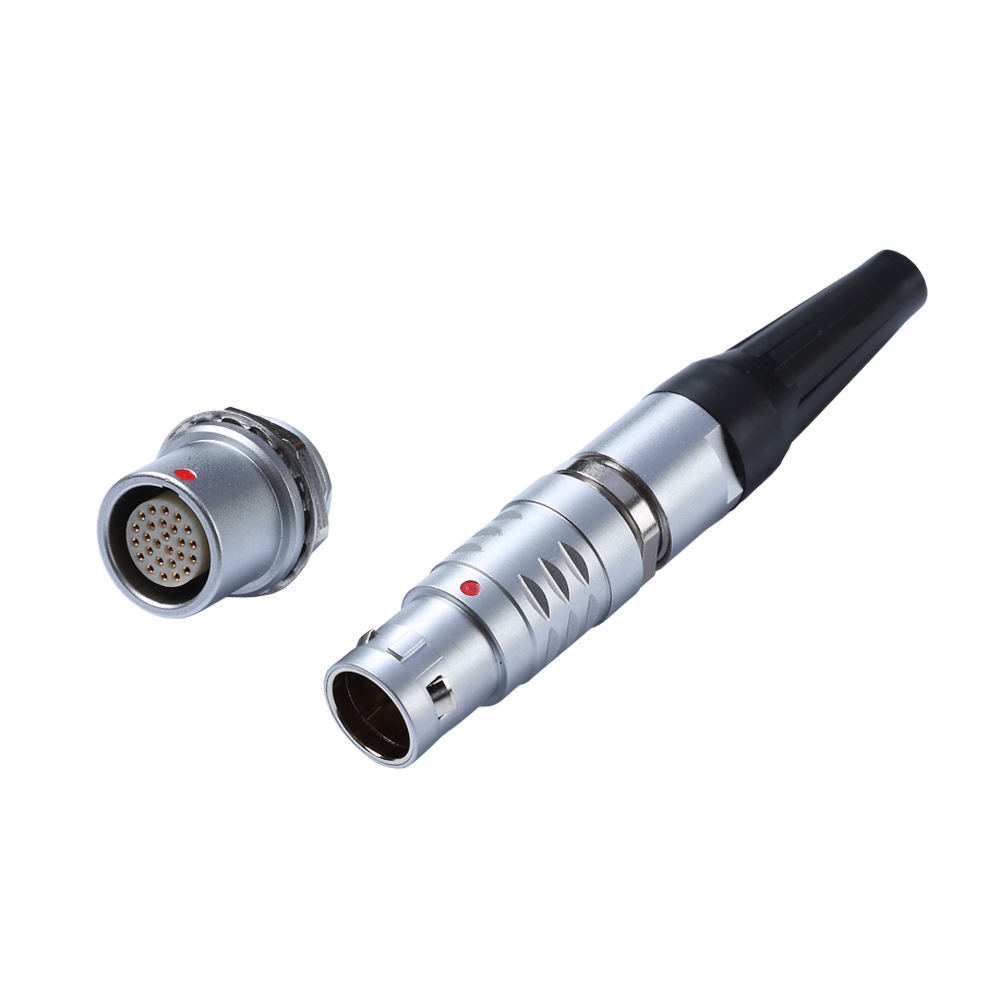
Every unplanned second of downtime in an advanced fab translates into lost yield, yet the connectors carrying power, signal, and gas through the most demanding process environments rarely get the attention they deserve. The right partner does more than ship components: they engineer for thermal shock, corrosive chemistries, and the kind of vibration that quietly kills inferior parts. At REUNION, that discipline shapes everything from material selection to traceability, because a connector is only as reliable as the questions asked before it reaches the cleanroom. Here are the qualities that separate suppliers who keep advanced fabs running from those who simply fill a bill of materials.
A Single Contact Failure Can Put a Whole Tool Bay on Hold
Tool bays rarely stop for dramatic reasons. More often, the culprit is a single contact that has worn just enough to break a sense line, drop a rail voltage, or send an intermittent interlock signal. What makes it frustrating is how small the failure looks next to the idle equipment around it: a pin with slight fretting, a connector with one loose socket, a probe tip dulled beyond its usable radius. Until that one contact is found, the entire bay sits dark.
The problem compounds because contact failures tend to be load-sensitive and temperature-sensitive. A pin may pass a cold continuity check, then open under thermal expansion once the chamber heats up. A marginal socket can deliver clean signals during slow diagnostics but collapse under normal data traffic. This behavior pushes technicians toward replacing expensive boards or rechecking software when the real fault is hidden in a mating surface that no longer makes consistent contact.
The practical fix is less about replacing everything and more about respecting contact life. Logging mating cycles, measuring low-level contact resistance under load, and checking for uneven wipe marks catch most failures before they strand a bay. When a tool does go down, the fastest recovery often comes from isolating the smallest common path first, because one bad contact has a way of looking like a far larger system fault.
Materials That Do Not Creep After Repeated Furnace Cycles
In a furnace that cycles between room temperature and 1200°C every few hours, most metals start to show creep long before they approach their melting point. The parts that survive without deforming are usually the ones with strong covalent or ionic bonding and a microstructure that does not coarsen much under repeated heat. Alumina, silicon carbide, and some grades of zirconia fall into this group because their atomic movement is negligible under normal furnace loads, so they retain flatness and alignment through hundreds of cycles.
For metallic components in vacuum, hydrogen, or inert gas, the choice narrows to refractory metals such as molybdenum, tungsten, and tantalum. These are not immune to creep, but their recrystallization temperatures are high enough that a support rod or heating element can stay straight for years if the atmosphere is kept oxygen-free and the load is well below the material's high-temperature yield strength. Oxidation, not gradual elongation, is usually what ends their service life.
A more useful way to judge these materials is to measure them after a cycle rather than rely on handbook data. A setter that has crept will show a visible crown or a change in slot width, while a stable one returns to nearly the same dimensions even after repeated soak-and-quench steps. That kind of long-term dimensional discipline is what keeps furnace tooling from becoming the hidden source of part distortion.
Vibration Tolerance That Protects Wafer Handling Accuracy
In wafer handling, the real challenge is not eliminating vibration entirely but defining a tolerance band that keeps placement errors below the point where they affect downstream yield. An end effector moving across a load port can easily transmit small oscillations into a 300 mm wafer, and even sub-micron relative motion at the contact interface can shift the wafer before the vacuum settles. The acceptable vibration level is therefore tied to what the lithography or inspection tool can absorb without losing overlay or focus accuracy.
Practical designs rely on stiff but well-damped arm structures, tuned acceleration profiles, and isolation of high-frequency motor ripple. Instead of simply adding mass, engineers often place natural frequencies of the handling mechanism away from known excitation bands so that resonance does not amplify a minor disturbance. In thin-wafer processes, this tolerance becomes tighter because a 50 µm substrate has far less inherent rigidity and can flex under vibration that a standard wafer would ignore.
At the tool interface, brief settling windows are built into the handoff sequence, allowing residual motion to decay below a measured threshold before clamps or pins release. This threshold is usually defined by accelerometer data or laser displacement feedback rather than by feel, and it is adjusted for wafer thickness, surface film stress, and transport speed. Keeping vibration inside that protective envelope preserves edge integrity and prevents the kind of subtle misalignment that only appears later as reduced die yield.
Contact Design That Keeps Signal Paths Quiet Next to RF Plasma
A quiet signal path next to an RF plasma source rarely comes from a single design choice. The plasma generator, match network, and chamber return currents create intense near-field coupling, and a poorly shaped contact can act as an unintended pickup loop or rectifying junction. The first step is usually to give the return current a predictable, low-inductance route so that the contact interface does not become the highest impedance point in the chain.
The mechanical interface itself matters more than its static resistance suggests. Multi-finger contacts, spring-loaded ground wipers, and RF gaskets work only when they maintain continuous shield coverage around the full circumference of a connector. Gaps or uneven normal force let the outer shield behave like a slot antenna, and small variations in contact resistance under thermal cycling can mix plasma noise into lower-frequency signal bands. Choosing contact plating and wiping geometry for long-term stability keeps that nonlinearity below a level where it corrupts analog readings.
Layout around the contact is just as critical. Ground via stitching immediately around a shielded connector reduces loop area and prevents return currents from spreading across the board. Sensitive analog front ends are best placed away from the main RF return path, with separate ground islands or buried reference layers to keep plasma-related transients out of low-level circuits. In many designs a common-mode choke or ferrite at the connector input proves necessary, but it is more effective when the contact shell itself provides a 360-degree termination rather than a single drain wire. Validation under real plasma ignition and pulse conditions usually reveals noise floor or phase noise issues that static continuity testing misses.
Mating Cycles That Match Real Maintenance Schedules
Field maintenance rarely follows the neat intervals printed in a product brochure. In practice, crews open panels, swap modules, and reseat connectors according to shutdown windows, production demands, or seasonal workloads. A mating cycle rating only becomes useful when it reflects how often those interruptions actually happen. If a connector is rated for 200 cycles but gets unplugged twice a month for inspection, it will hit that limit far sooner than the equipment’s expected service life.
The mismatch usually shows up in one of two ways. Overspecified parts add cost without adding value, because a 10,000-cycle contact may never see more than a few hundred separations before the whole assembly is retired. Underspecified parts create a different problem: the plating wears thin, contact resistance creeps upward, and intermittent faults begin appearing right around the time the facility is busiest.
A better approach is to build a simple count from the actual maintenance plan. List every scheduled inspection, calibration task, filter change, and module swap that requires breaking a connection. Then add a realistic margin for unscheduled troubleshooting. That total gives a cycle figure tied to the way the equipment is really maintained, making it easier to choose connectors that survive long enough without paying for durability nobody needs.
Vendor Support That Knows the Difference Between Ramp and HVM
When you're pushing a product from the early prototype stage into a hard ramp, the support questions change fast. One week it's about firmware quirks on a handful of boards, the next it's about yields, test coverage, and whether the supply chain can hold up at 5x volume. Most vendors treat every escalation the same way, but the ones worth keeping know the difference between a lab problem and a line-down situation.
Ramp means the tolerances you thought were fine start showing up as field failures, and suddenly you need someone who can read a pareto chart without asking what it is. HVM means the discussion shifts from "can we fix this batch" to "how do we prevent this across three shifts and two fabs." A support team that gets this won't waste your time walking through basic bring-up steps when you've already shipped a hundred units. They'll ask about your DPPM targets, your ICT coverage, your burn-in duration—the things that actually move the needle.
That's the real threshold: not whether they can answer a ticket, but whether they can tell you which risks are still acceptable at your current stage and which ones will kill your ramp schedule. If a vendor's first response to a yield dip is a link to a generic knowledge base article, you're already behind. The ones who know the difference between ramp and HVM come back with a specific experiment plan and a list of likely suspects before you've finished your coffee.
FAQ
Trust usually comes down to how a supplier handles deviations. A fab doesn't want surprises after a process change, so the best connector companies document every resin lot, plating bath, and cure cycle and notify the customer before anything shifts. They also tend to have application engineers who understand vacuum, RF, and aggressive chemistries, not just catalog parts.
Connectors inside process tools sit next to harsh gases, plasmas, and repeated thermal swings. A housing that looks fine on a bench can outgas in vacuum or turn brittle after exposure to fluorine-based cleaning chemistry. Suppliers that keep advanced fabs running qualify materials for low outgassing, ESD safety, and resistance to specific etch and deposition byproducts rather than relying on generic industrial plastics.
They provide more than a data sheet. Expect ion chromatography reports, outgassing test results, particle counts, and cleanroom packaging records. Some suppliers also run bake-out cycles before shipment and double-bag parts in nitrogen-flushed film. That level of documentation lets a fab trace a particle excursion back to a specific lot instead of guessing.
Standard circular connectors often can't handle the mix of high pin counts, tight bend radii, and low-profile mounting inside modern chambers. A capable supplier will modify contact spacing, build hybrid signal/power layouts, or redesign strain relief without forcing the fab to re-qualify the entire subsystem. The value isn't just the drawing; it's managing the change so the tool stays within its existing process window.
Because one mixed lot can shut down a line while engineers hunt for the source of a yield drop. Advanced fabs now expect lot-level traceability from raw polymer to finished assembly, including subcomponents like contacts and O-rings. If a supplier can't provide that chain, the fab has to treat every installed connector as suspect during an investigation, which costs far more than the part itself.
The strongest suppliers run buffer stock near major fab clusters, offer consignment programs, and maintain duplicate tooling for high-runner part numbers. They also share capacity forecasts early enough to reserve plating and molding time. It's less about promising fast shipping and more about absorbing demand spikes without forcing the fab to redesign around a shortage.
Beyond basic continuity and hipot tests, wafer handling connectors typically need thermal cycling, vibration, flex-life validation for moving cables, and exposure to the specific cleaning solvents used in the fab. Some applications also require low-force mating verification to avoid particle generation from contact fretting. A supplier with in-house test labs can usually shorten that qualification by running standard sequences and reporting data in the fab's preferred format.
Rarely without compromise. Etch tools may need high-temperature and aggressive chemical resistance, deposition tools may care more about high current and vacuum compatibility, and metrology tools often prioritize signal integrity and low particle shedding. A thoughtful supplier will offer a platform with shared tooling and mixed layouts, but they won't claim a single part number solves every chamber requirement.
Conclusion
A connector problem in an advanced fab rarely announces itself. More often, a single worn contact takes down a process tool, and the entire bay slows while maintenance pulls a module nobody expected to touch until the next scheduled PM. That is why the first thing equipment teams look for is a supplier that treats contact force as a long-term variable, not a datasheet constant. Materials must hold their shape through repeated furnace cycles instead of creeping and relaxing after thermal stress. The connector body also has to live with constant micro-vibration from wafer handling robots and cryo or vacuum pumps; if it loosens even slightly, plating wear follows and the electrical path starts to degrade. In chambers sitting next to RF plasma, the shielding and contact geometry need to keep signal paths quiet, because once noise couples into a sensor line the tool may chase ghosts instead of wafers.
Mating cycles matter just as much as headline specifications. A connector rated for a thousand clean insertions may look acceptable in a qualification report, but if it cannot survive the insertion count of real maintenance schedules, it becomes a hidden cost during every rebuild. The right design accounts for how the tool is actually serviced, including partial disconnects and repeated reseating in less-than-clean conditions. Beyond the hardware, vendor support has to recognize the gap between ramp and high-volume manufacturing. Ramp customers need rapid feedback, small lots, and engineers who can help debug first integration issues. HVM customers need locked processes, lot traceability, and no surprises when volumes climb. Suppliers that understand both phases without blurring them are usually the ones that keep advanced fabs running.
Contact Us
Contact Person: Hayley Liang
Email: [email protected]
Tel/WhatsApp: +86 13480625451
Website: https://www.reunion-china.com/