Threaded Reinforcing Bar Socket Manufacturer Essential Selection Criteria
2026-10-19
Selecting a threaded reinforcing bar socket manufacturer isn’t just about price per unit. It’s about tensile strength, thread consistency, material traceability, and whether the supplier can actually deliver on time—every time. Miss one of these, and the strongest rebar layout can underperform at the joint. That’s why we’re breaking down the essential criteria, and why Sinou keeps showing up in shortlists for projects that can’t afford guesswork.
Material Traceability That Goes Beyond a Mill Certificate
A mill certificate only tells you the batch chemistry and the date it left the furnace. It says nothing about the path that bar took through the warehouse, the hand that loaded it, or the truck that carried it across three state lines. Real traceability means being able to pull up a heat number and see the entire journey: every lift, every transfer, every signature. That’s the difference between a piece of paper and a living record.
We don’t stop at the certificate. Each heat is assigned a digital thread that follows the material from the mill’s pour to the final cut on the shop floor. Operators scan, verify, and timestamp at every touchpoint, so a bar sitting on your rack isn’t just “certified” — it’s accounted for. If a recall happens, you don’t spend days hunting through file cabinets. You search one number and see exactly which parts of your inventory came from that specific coil or plate.
The real value shows up when things go wrong. A customer calls with a failed part at 2 a.m. Instead of guessing, you trace the material back through forming, heat treating, and machining. You find the exact coil, the exact shift, and the exact piece of equipment that ran it. That’s not just compliance — that’s control. And it’s why we treat a mill certificate as the floor, not the ceiling.
Thread Geometry Checks You Can Perform Before Purchase
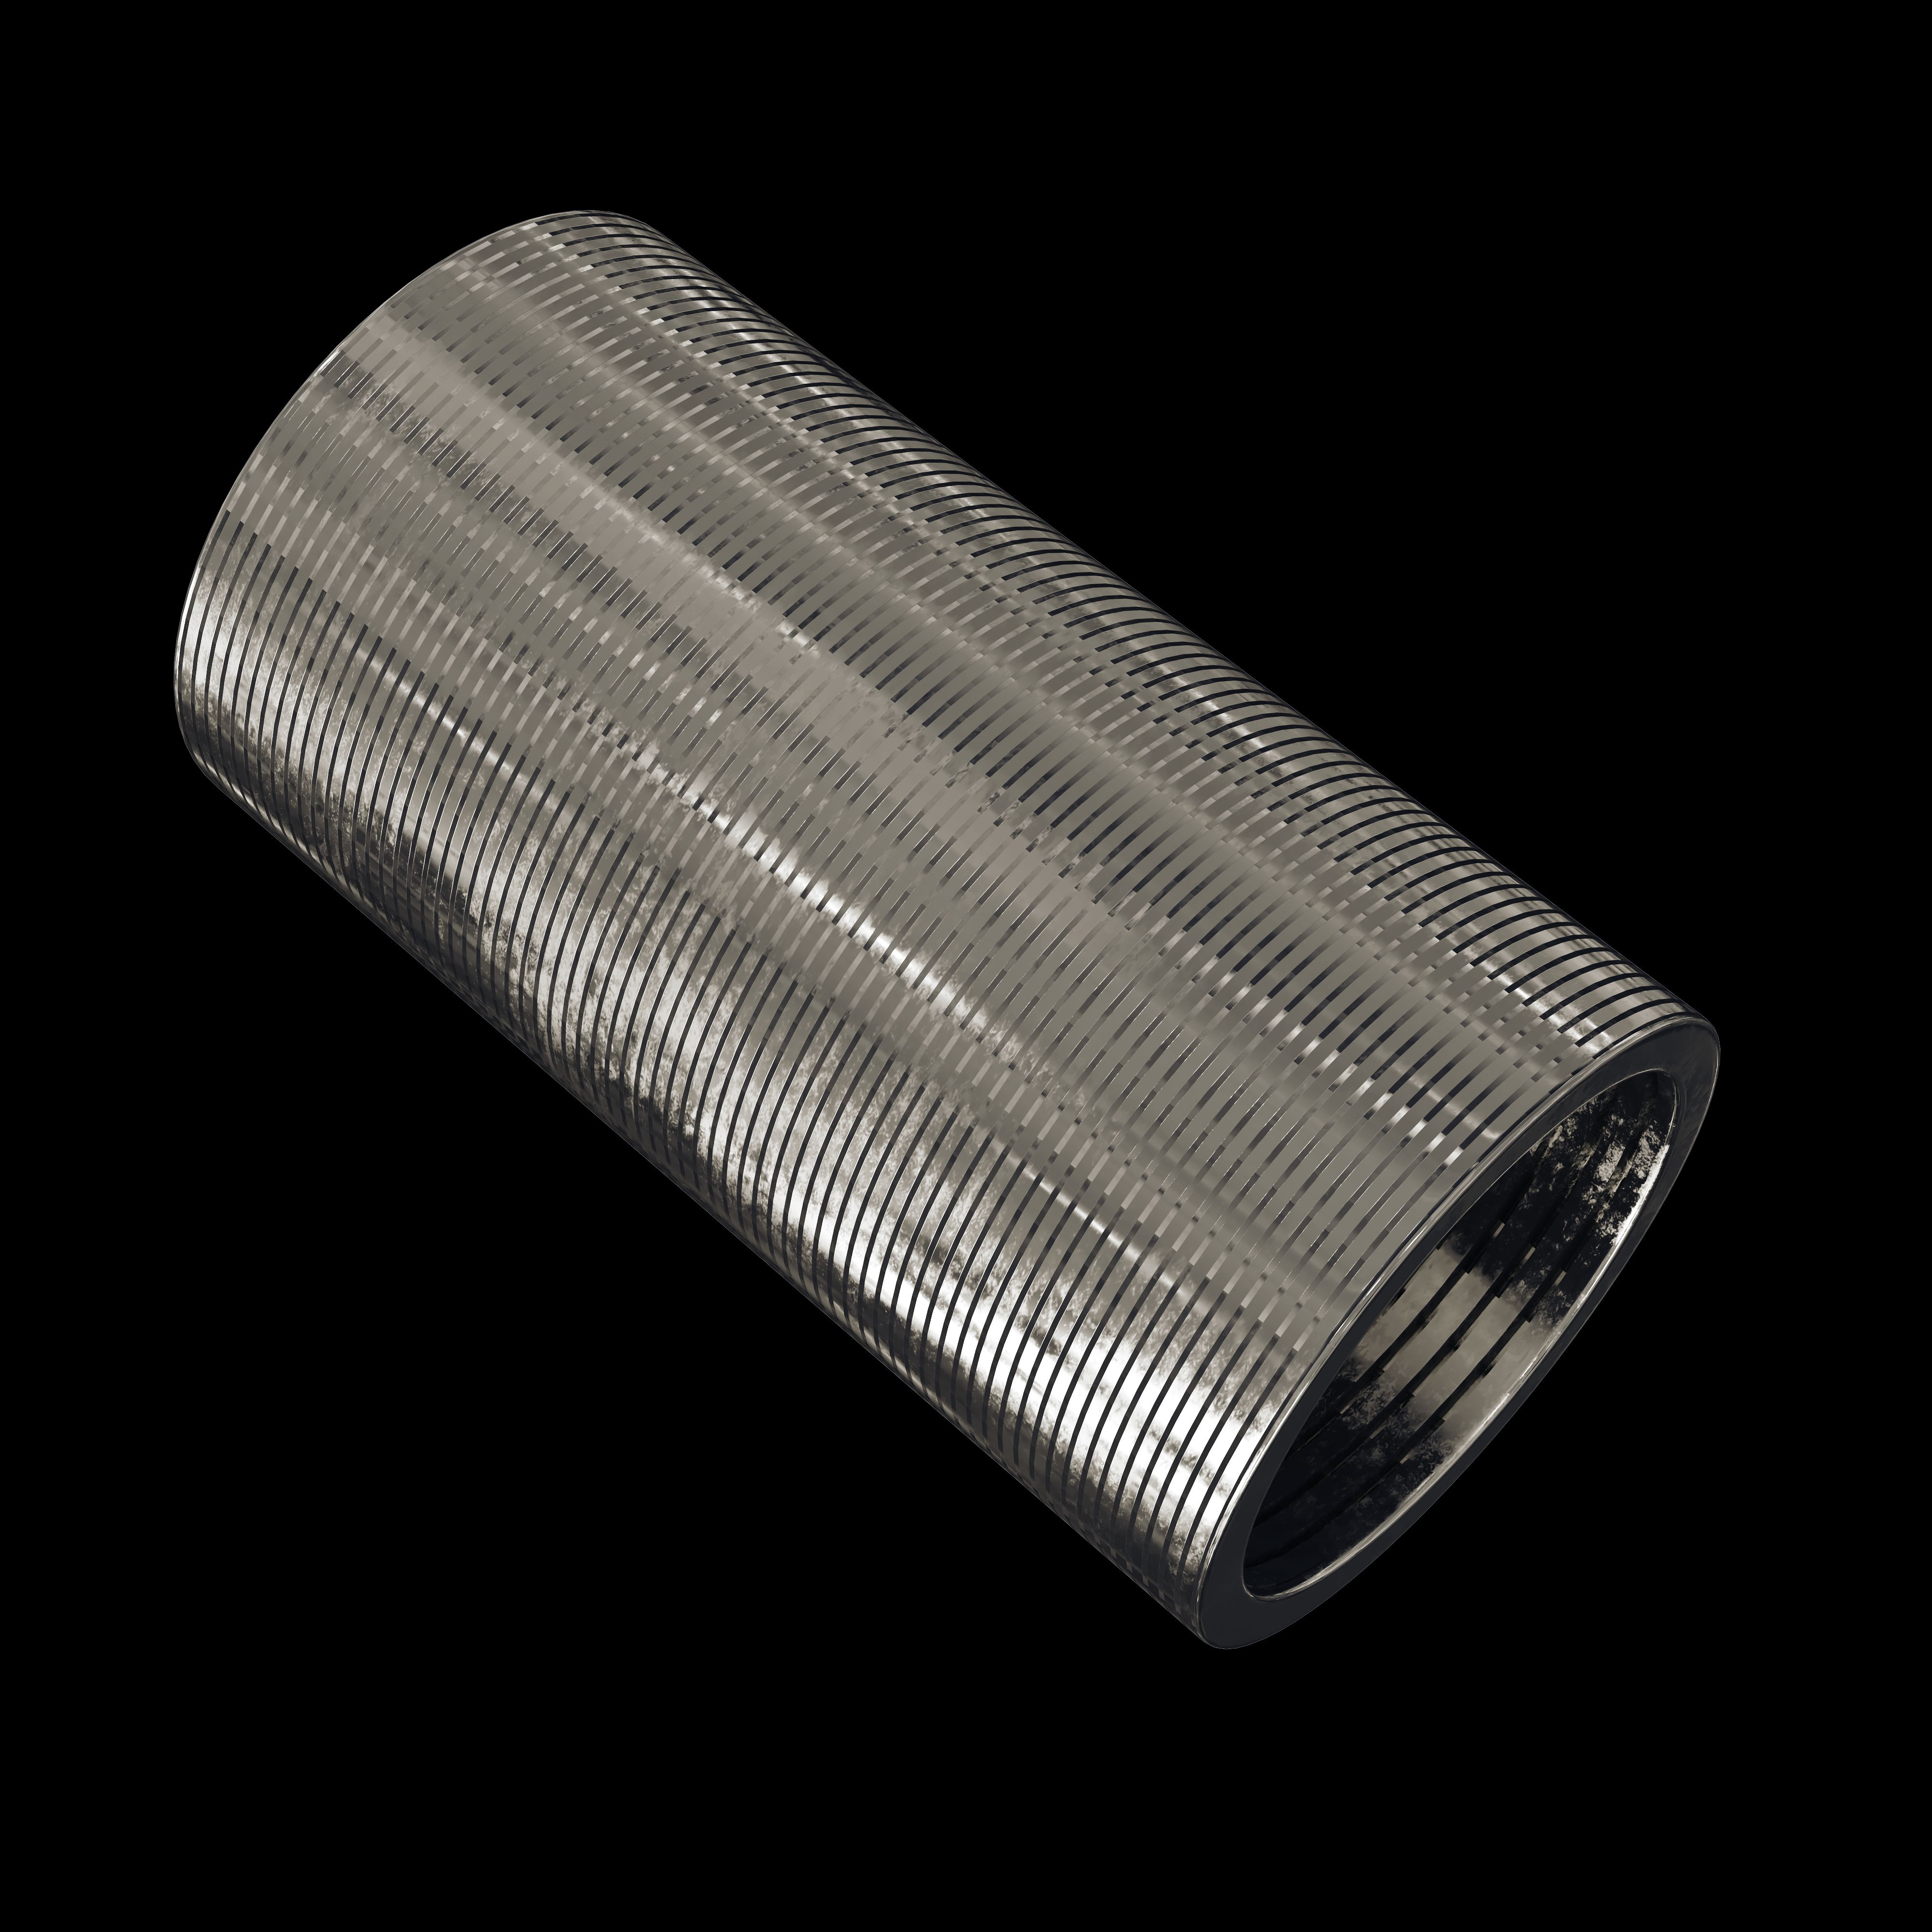
Thread geometry rarely gets the attention it deserves until a fastener seizes or a fitting leaks under pressure. Before committing to a purchase, grab a thread pitch gauge and a set of go/no-go gauges. Check the pitch diameter first—if the crests look sharp or the roots appear overly flat, the thread was likely cut with worn tooling or on a machine that hasn't been calibrated recently. A quick visual sweep under a magnifier can reveal torn flanks, inconsistent helix angles, or plating that's built up unevenly in the valleys.
Don't stop at the diameter. Run your fingernail along the flank of a sample thread; you shouldn't feel chatter marks or a sudden change in lead. Measure the major and minor diameters against the spec sheet, especially on the first and last full thread, since those are the zones where cutting tools enter and exit and often leave behind a mismatched form. If the vendor allows it, thread a mating part by hand—excessive wobble or binding in the first two turns usually points to a lead error, not just a tight tolerance.
Plated or coated threads deserve an extra step: ask for a pre-plating dimensional report or measure a few threads before coating is applied. Because a uniform coating thickness doesn't translate to a uniform pitch diameter change, especially on fine-pitch threads. If the supplier can't provide that data, it's worth buying a small sample batch first and checking the functional diameter with a ring gauge after plating.
Independent Load Testing: Why Manufacturer Claims Aren't Enough
When a manufacturer publishes load ratings for their products, those numbers come from controlled environments that rarely reflect real-world conditions. Temperature fluctuations, uneven weight distribution, and years of wear can all chip away at performance in ways that factory tests simply don't account for. Independent load testing strips away the marketing gloss by pushing equipment beyond its advertised limits under unpredictable, messy conditions—the same conditions your operation faces every day.
Think about the last time a shelf, pallet rack, or lifting sling failed unexpectedly. Chances are the failure didn't trace back to a single overloaded moment, but to a slow accumulation of stress from repeated cycles, minor impacts, and environmental exposure. Manufacturer specs are often derived from one-time destructive tests on brand-new samples, which tells you little about how that same component will behave after five years of daily abuse. Independent testing fills that gap by simulating fatigue, aging, and real-world abuse patterns.
Relying solely on factory claims also creates a dangerous blind spot when you're comparing products from different brands. Without a standardized independent benchmark, one company's "safe working load" might be calculated with a massive safety factor while another's is razor-thin. Third-party load testing gives you an apples-to-apples comparison and exposes weak points that a glossy brochure will never mention. In the end, it's about protecting your people, your inventory, and your downtime costs—not just trusting a sticker.
Corrosion Protection Options Matched to Site Conditions
Site-specific variables drive coating choice. For coastal or marine environments, high chloride deposition and prolonged wetness demand zinc-rich primers and high-build epoxy or polyurethane topcoats; in contrast, inland arid regions with intense UV may favor polysiloxane finishes that resist chalking. Buried steel in acidic or high-moisture soils often requires a combination of factory-applied fusion-bonded epoxy and sacrificial anodes or impressed current cathodic protection, sized after soil resistivity and pH are measured.
Matching protection to conditions also means accounting for microclimates around the structure. Areas shielded from rain but exposed to industrial fallout may accumulate corrosive salts and need more frequent inspection or a thicker barrier coat. For water tanks and pipelines, internal corrosion from soft or high-chloride water can be addressed with cement mortar lining or epoxy linings rated for immersion. Rather than applying a generic system, field surveys—including atmospheric corrosion rate coupons and soil or water sampling—help select a balance of coating, wrapping, and electrochemical protection that fits the local stressors without over-engineering.
Supply Chain Resilience: Avoiding Delays That Stall the Pour
When a concrete pour is scheduled, every hour of delay ripples through the project like a crack spreading across fresh cement. The real culprit is rarely the mixer truck breaking down on the highway—it's the fragile web of suppliers, sub-tier vendors, and last-minute substitutions that quietly unravel under pressure. Resilient teams map their entire material flow weeks ahead, identifying which single-source aggregate or admixture could derail the pour if a plant loses power or a batch fails testing. Instead of relying on one backup plan, they build layered buffers: pre-qualified secondary suppliers within a two-hour radius, on-site storage for critical additives, and clear trigger points for switching to an alternative mix design without waiting for approval chains.
What separates teams that pour on schedule from those that watch the slump drop while arguing on the phone is how they treat the final 48 hours. A resilient supply chain doesn't just track purchase orders—it verifies that raw materials have actually left the quarry, that the batch plant has enough fly ash for the full day's volume, and that the pump operator's fuel contract covers overtime. The best practice is a live checklist owned by one person, not a shared spreadsheet that everyone glances at. When a truck is 20 minutes late, that person already knows whether to reroute from a neighboring job site or shift the pour sequence to start with footings instead of walls. That kind of micro-decision, made from real-time visibility rather than panic, keeps the crew productive and the concrete within spec.
Long-term resilience comes from treating supply chain failures as design data, not just bad luck. After each delayed pour, a short debrief should document which assumption broke first: was it a supplier's capacity promise, a weather window that closed faster than forecasted, or a quality hold that no one communicated upstream? Those patterns become the basis for contract language that ties bonuses to verified readiness rather than paper confirmations. It also means building relationships with smaller, local batch plants that can produce smaller volumes on short notice—often at a premium, but far cheaper than the cost of tearing out a cold joint or paying a full crew to stand idle. Over time, this turns a reactive scramble into a repeatable playbook, where avoiding delays isn't a heroic save but the default rhythm of the job.
Field Support and Training That Prevent Costly Rework
Rework often starts with a small misread of site conditions or a crew that hasn't seen a particular installation detail before. Field support that puts experienced technicians on the ground changes that equation. Instead of waiting for a phone call after something goes wrong, they walk the site, catch alignment and clearance issues early, and show installers how to handle the tricky transitions that aren't obvious from drawings. That kind of direct intervention stops mistakes before they harden into expensive tear-outs.
Training works best when it's built around the actual tools and materials the crew will use on the job. Short, focused sessions on torque settings, flashing sequences, or joint prep give people a chance to ask the questions they'd otherwise guess at. When a trainer can point to a specific bracket or sealant and explain the failure mode it prevents, the lesson sticks. Crews leave with better muscle memory and fewer assumptions, which means fewer callbacks and less wasted material.
The payoff shows up in the schedule and the budget. Jobs with early field support tend to hit inspection the first time because the work meets spec before the inspector ever arrives. When training covers the common failure points - penetrations, terminations, load paths - teams stop improvising. That consistency reduces the sort of rework that eats into margins and delays handover.
FAQ
Ask for the mill certificates for the steel used in their sockets, not just a generic material data sheet. Also request third-party fatigue test reports that match the specific thread profile you plan to use. A manufacturer that hesitates to share these documents usually has something to hide.
Look for ISO 9001 as a baseline, but don't stop there. For critical projects, check if they can provide product-specific approvals like ACI or local building code compliance. CE marking or equivalent regional certification also helps if you're sourcing across borders.
Thread geometry controls how evenly load transfers between the bar and socket. If the pitch or flank angle is slightly off, you get stress concentrations that lead to premature failure under cyclic loading. A manufacturer that controls thread form with dedicated gauges and regular calibration is worth prioritizing.
Ask for raw test data from their last production batch, not just a glossy brochure claim. Reputable shops will have records of slip tests, tensile tests, and occasionally fatigue testing on assembled bar-socket systems. If they only test the socket in isolation, that's a warning sign.
Watch out for inconsistent thread fit across batches, missing heat numbers on parts, or an inability to explain their quality control process in detail. If they push price as the only advantage while avoiding technical questions, keep looking.
Local sourcing often gives you faster turnaround and easier site audits, but don't assume overseas means lower quality. The real question is whether the manufacturer's logistics and communication match your project's tolerance for delay. A nearby supplier with weak QC is worse than a distant one with rigorous process control.
A manufacturer's ability to hold buffer stock of common thread sizes can save your project from costly downtime. Ask about their typical lead time for non-standard diameters and whether they use a made-to-order or stock-and-ship model. Consistent delivery scheduling often trumps a slightly lower unit price.
Traceability links each socket back to its heat of steel, allowing you to track known material defects or recalls. If a manufacturer can't provide full traceability from raw bar to finished socket, you're taking on avoidable risk. It's especially critical for projects in seismic zones or marine environments.
Conclusion
Selecting a manufacturer of threaded reinforcing bar sockets demands more than checking a catalog. Start by verifying material traceability: request heat numbers, chemical composition reports, and third-party certifications that link each socket to the original steel batch, not just a generic mill certificate. Before committing, physically inspect thread geometry using go/no-go gauges, check pitch diameter and thread angle consistency, and ask for dimensional reports from multiple production runs. Independent load testing is non-negotiable—look for pull-out tests, cyclic fatigue data, and cyclic loading results from an accredited lab, not manufacturer self-declarations. These three checks form the backbone of mechanical reliability.
Equally important are field-level factors. Corrosion protection must match your site: hot-dip galvanizing for marine or buried use, epoxy coating for aggressive soil, or stainless steel for chemical exposure. Review the manufacturer's coating adhesion and thickness tolerances. Supply chain resilience means confirming raw material inventory levels, secondary production sites, and realistic lead times—ask for a contingency plan for logistics disruptions or raw steel shortages. Finally, insist on field support: on-site training for couplers, torque calibration guidance, and troubleshooting response times. A manufacturer that offers installation supervision and documented rework prevention procedures will save more money than any price discount.
Contact Us
Contact Person: HaiYan
Email: [email protected]
Tel/WhatsApp: +86 18957325588
Website: https://www.senyoubeton.com/